Explosion-Proof Drum Pump Motor Supports Hazardous Fluid Transfer
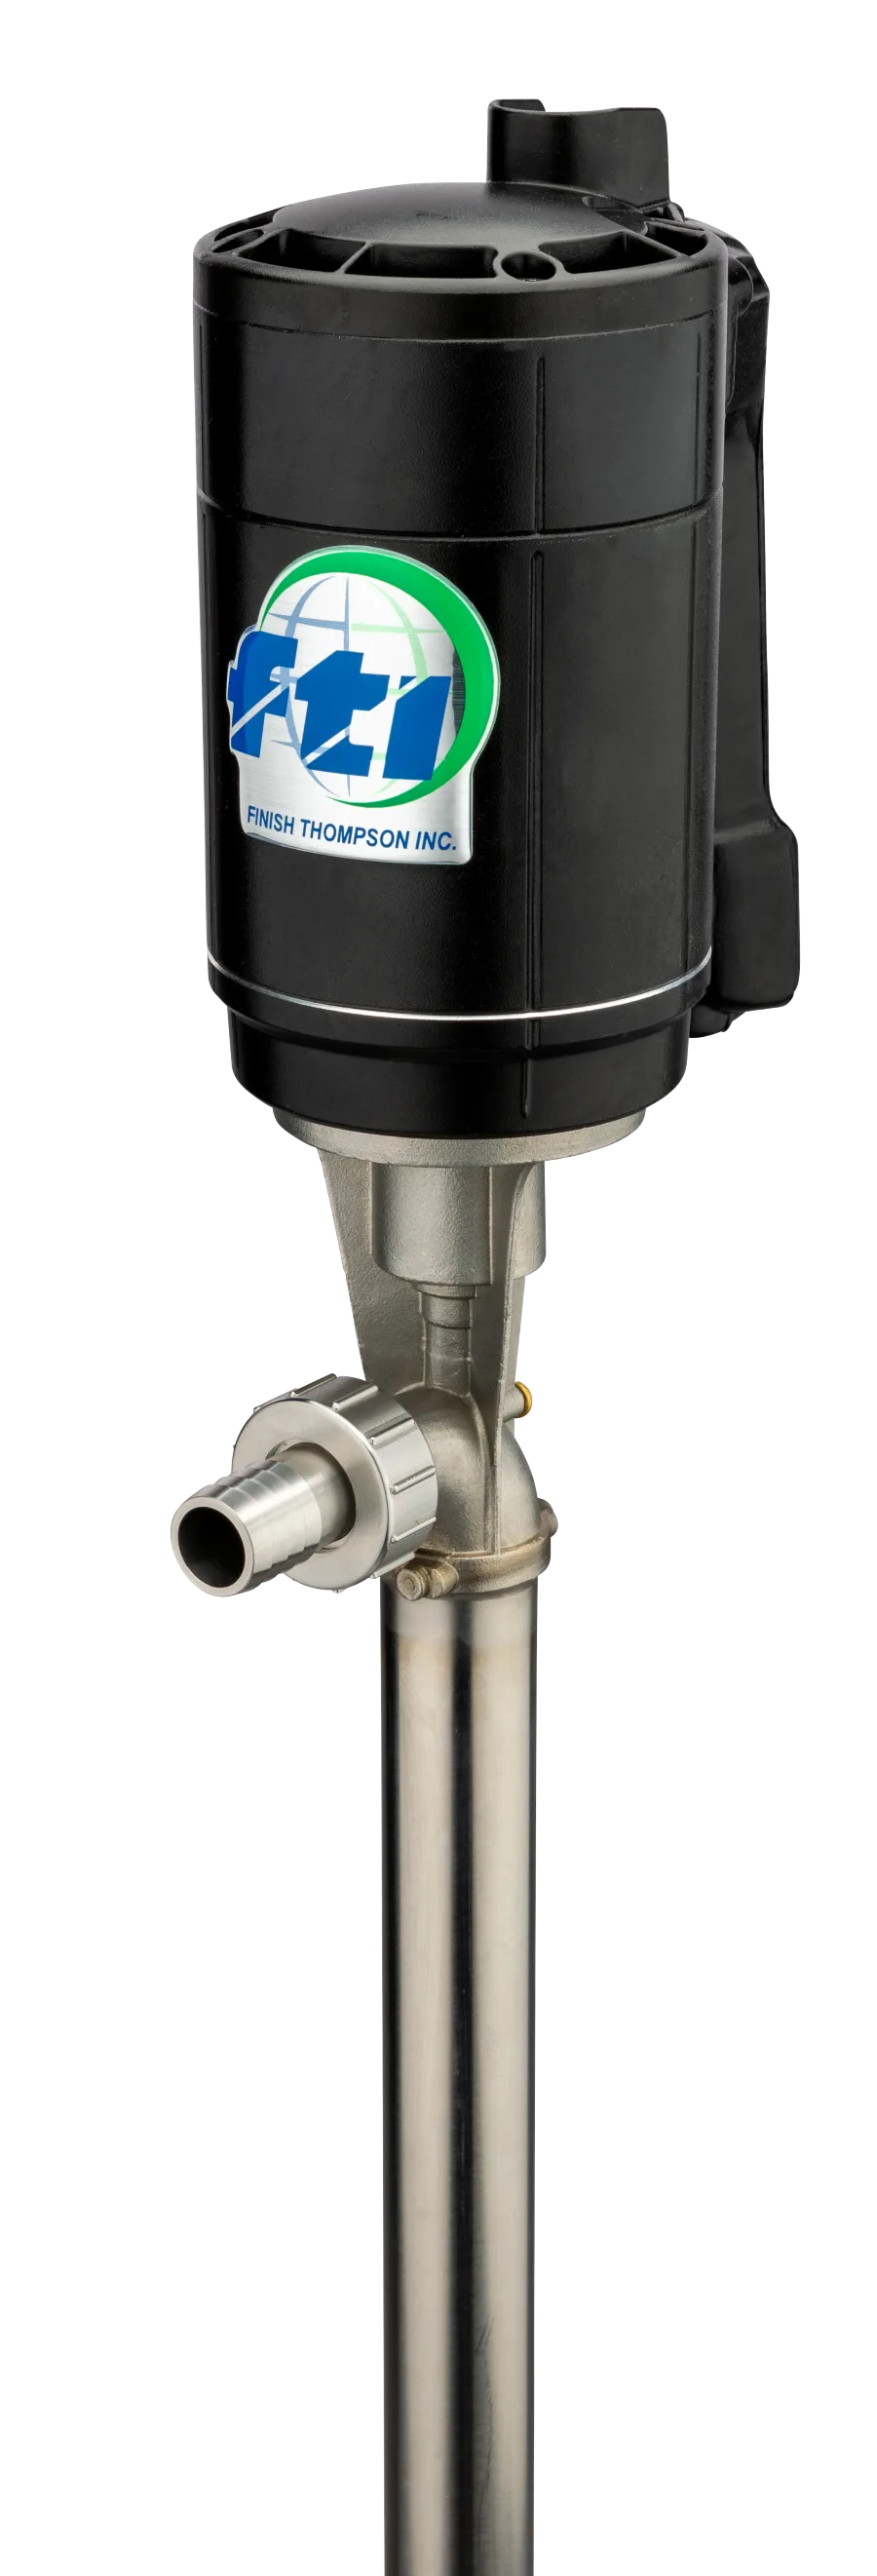
Finish Thompson Inc. has introduced its SX Series explosion-proof electric motor for drum and barrel pump applications involving flammable and combustible liquids.
Designed for use with the company's EFS Series drum and container pumps, the motor is intended for hazardous fluid-transfer environments requiring explosion-proof or flame-proof equipment.
The two-speed design provides flow rates of up to 17 gallons per minute at full speed and 7 gallons per minute at low speed when transferring nonflammable fluids.
For flammable or combustible liquids, the system supports flow rates of up to 4 gallons per minute.
According to the manufacturer, the motor can empty a 55-gallon drum in slightly more than three minutes under applicable operating conditions.
The lower-speed setting is intended to support controlled filling of smaller containers while reducing splashing.
The motor weighs approximately 6.6 pounds and is designed for continuous operation.
A built-in grounding lug allows the motor, pump tube and container to be bonded and grounded to help dissipate static electricity.
Three versions are available.
The S1X operates at 115 volts and is QPS certified for Class I, Division 1, Group D environments with a T3 temperature rating.
The S2X operates at 230 volts and carries international certifications including CE, ATEX and IECEx for applicable hazardous environments.
The S3X-HT is designed for elevated ambient temperatures up to 140 °F.
All versions include a 12-foot power cord.
Finish Thompson manufactures chemical-transfer equipment for industrial applications, including drum pumps, centrifugal pumps and air-operated double-diaphragm pumps.
Safe handling of flammable solvents and other chemicals is an important consideration in coatings manufacturing. Explosion-proof transfer equipment can support safer material handling and production operations.
Looking for a reprint of this article?
From high-res PDFs to custom plaques, order your copy today!